Automotive Relay Manufacturing: Meeting IATF 16949 Standards with Fully Automated Assembly Lines
-
Automotive Relay Production Line
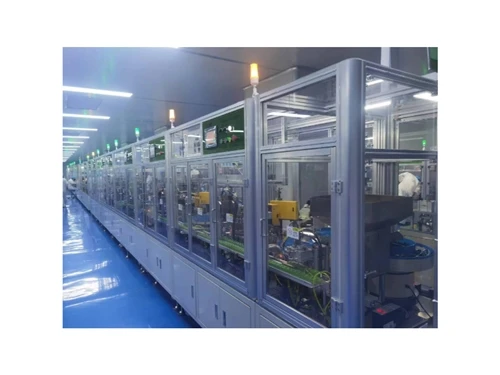
Automotive micro and high-current relays require full traceability and statistical process control per IATF 16949. This turnkey automatic assembly line completes base loading, yoke crimping, coil winding, contact assembly and dimensional inspection within 2.2s cycle time, with positioning repeatability ±0.005mm and Cpk≥1.67 for critical dimensions. It records every station data for PPAP and audit traceability.
-

Automotive Relay Production Line
-
Automotive Micro & High-Current Relay Requirements
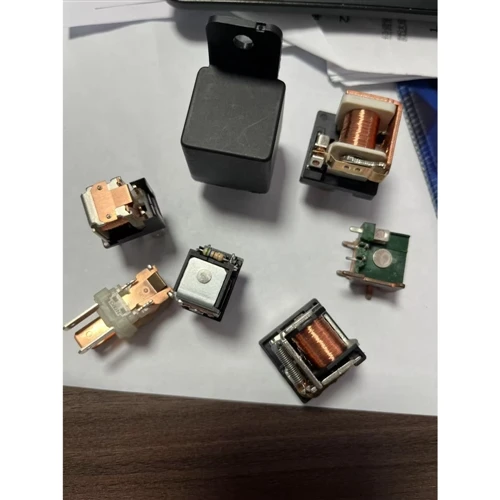
IATF 16949 mandates closed-loop part traceability, MSA validated measurement systems and containment for safety-critical relay components. Key controlled parameters include coil resistance, contact gap, terminal flatness and overall assembly height. Non-conforming parts must be automatically rejected without manual sorting.
Mechanical Poka-Yoke interlock prevents reversed or missing component loading. Telecentric machine vision verifies part orientation before assembly. Post-assembly height measurement uses laser displacement sensors, gauge R&R ≤10%. Any dimension out of spec triggers immediate part rejection and logs batch ID, station timestamp and measured value for traceability.
Micro relay
contact gap tolerance ±0.02mm, max 1.8s cycle time
High-current relay
axial crimp force 1200N, overload endurance test integration

Core Machine Breakdown: Base, Yoke, Coil Stations
| Station | Repeatability | Cycle Time | Actuation & Sensing |
|---|---|---|---|
| Base feeding station | ±0.01mm | 0.4s | Vibratory bowl + PPU pick and place unit |
| Yoke crimping station | ±0.005mm | 0.6s | Closed-loop servo riveting, force-displacement envelope monitoring |
| Coil winding station | ±0.008mm | 0.7s | 20000RPM spindle, wire tension closed-loop control |
| Contact assembly station | ±0.005mm | 0.5s | Anti-backlash ball screw drive |